Buyers see the finished part. Factory teams also manage the handovers, checks and small decisions that determine whether the result stays stable in repeat production.
Quick Answer
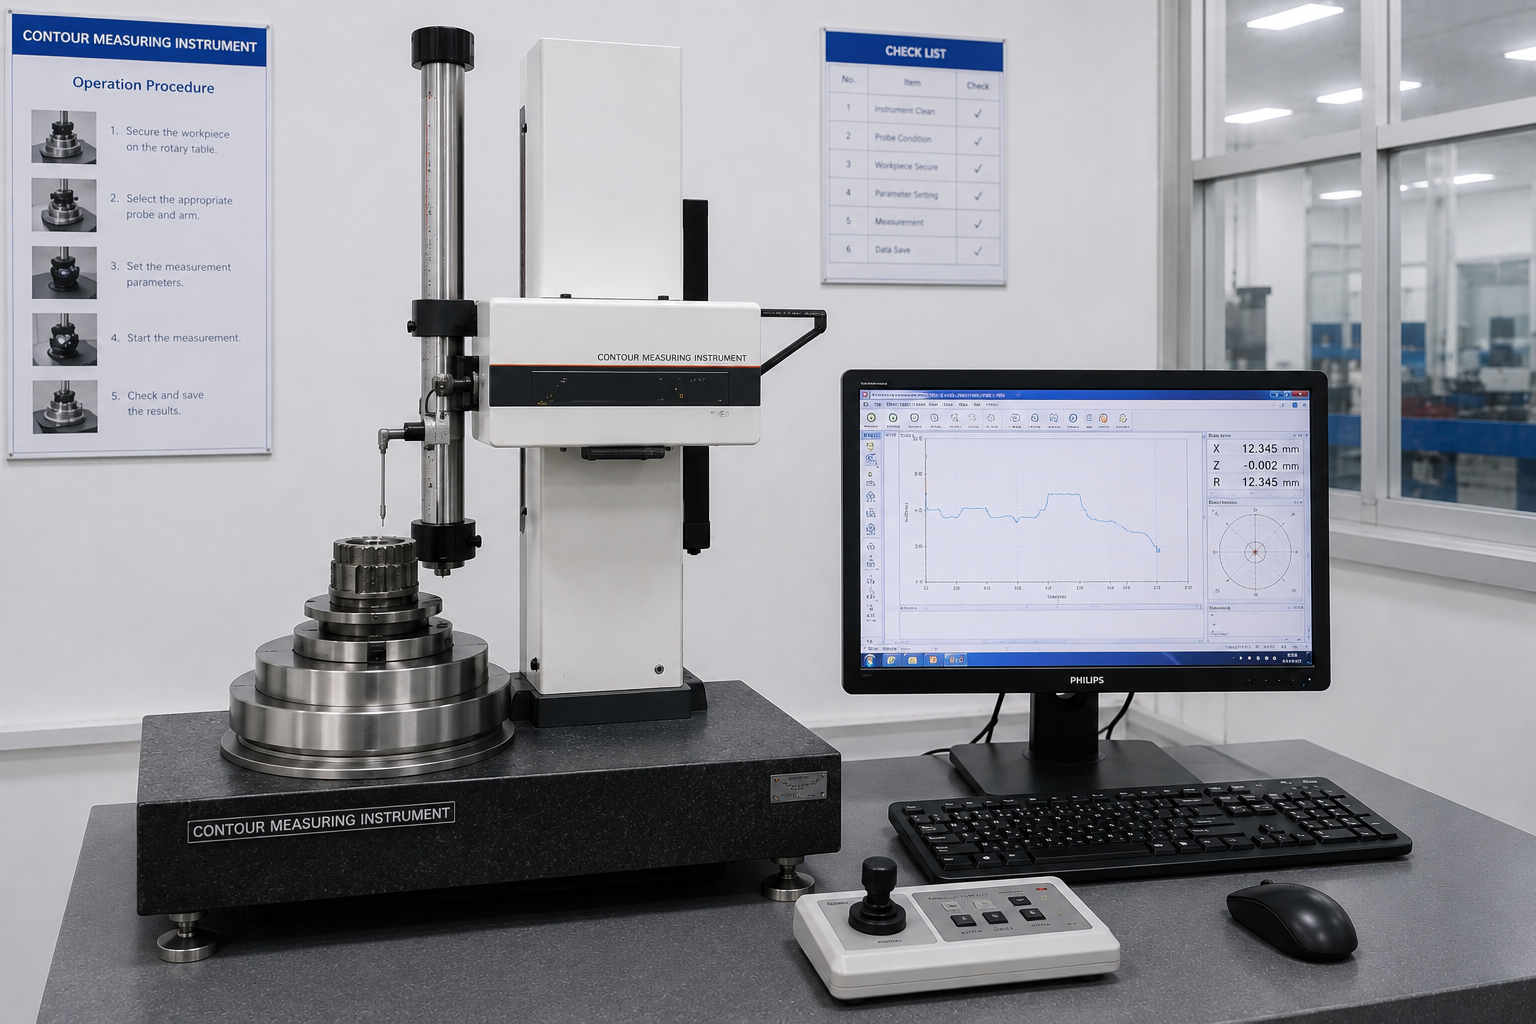
Use a CMM when you need recorded coordinates, geometry or a flexible dimensional report. Use a go/no-go gauge when a defined feature can be checked quickly and repeatably at production. Many projects use both.
A Detailed Report That Arrived Too Late
A low-volume part received a complete dimensional report after inspection, but the assembly line needed a quick check during production. The report was useful for approval; it was not the right tool for every in-process decision.
Match the Tool to the Question
A CMM can describe where a feature is. A gauge can quickly answer whether a feature falls within an agreed limit. Do not use a slower method where a controlled production check is enough.
Consider Datum and Loading
A gauge still needs consistent locating and contact. A CMM still needs a suitable fixture and measurement strategy. Tool name alone does not guarantee a reliable result.
Use Reports for Learning
CMM data can help identify drift, tool wear or process capability. A gauge can support rapid reaction when the process is stable and the limit is clear.
Control Gauge Wear
A production gauge must have an identification, checking interval and reaction plan. A worn gauge can create false confidence just as a worn cutting tool can change the part.
Nbfeiyu Factory View
Nbfeiyu selects measurement methods around the characteristic and production risk, linking inspection records with machining, molding and assembly controls.
Buyer Checklist
- Define the feature and inspection question.
- Confirm datum, locating and loading method.
- Set the required report detail and frequency.
- Check gauge identification and wear control.
- Use a functional check where dimensional proof is incomplete.
- Define reaction limits for failed results.
FAQ
Is a CMM always more accurate?
A CMM can provide detailed data, but accuracy depends on calibration, fixture, probing strategy, environment and the characteristic being measured.
Can a gauge replace a CMM report?
A gauge may support production checks, but it does not replace a dimensional report when coordinate data or geometry evidence is required.
Should buyers specify the instrument by brand?
It is usually better to define the required accuracy, method and evidence, then let the factory propose suitable calibrated equipment.
Conclusion
CMMs and go/no-go gauges serve different inspection decisions. Choose the method around the feature and production risk, then control fixtures, gauge condition, records, and reaction limits so the result remains useful.
Need Help With This OEM Project?
Send the drawing, critical dimensions and expected inspection frequency. Nbfeiyu can recommend a practical CMM, gauge or combined inspection route.